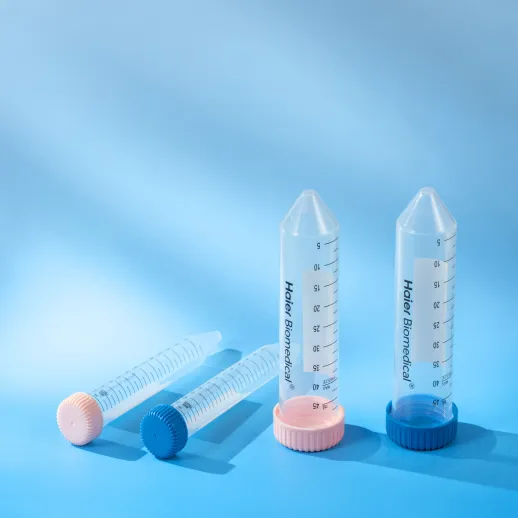
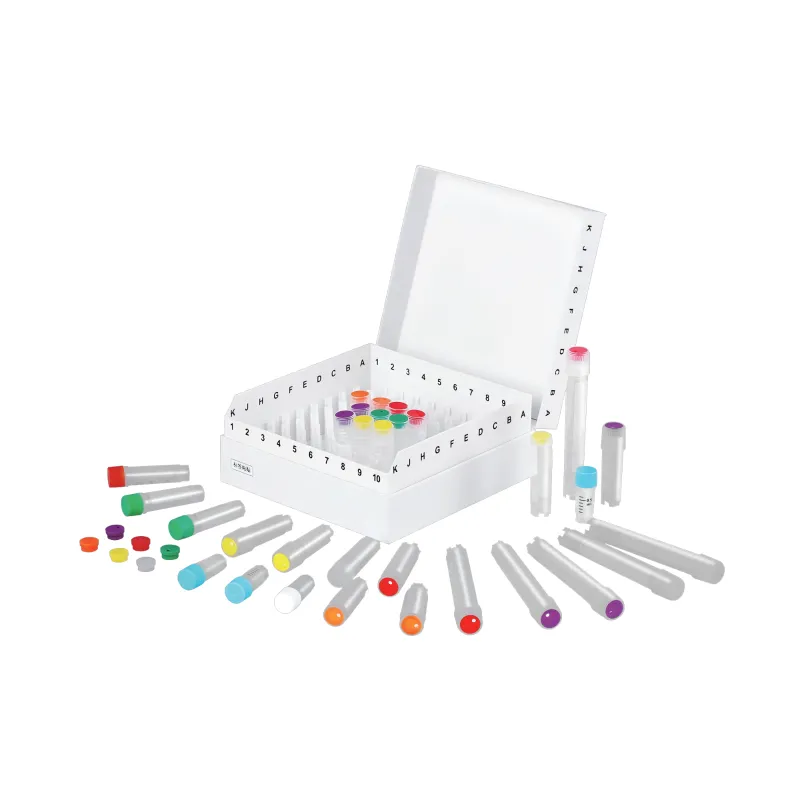
polypropylene microfuge tubes
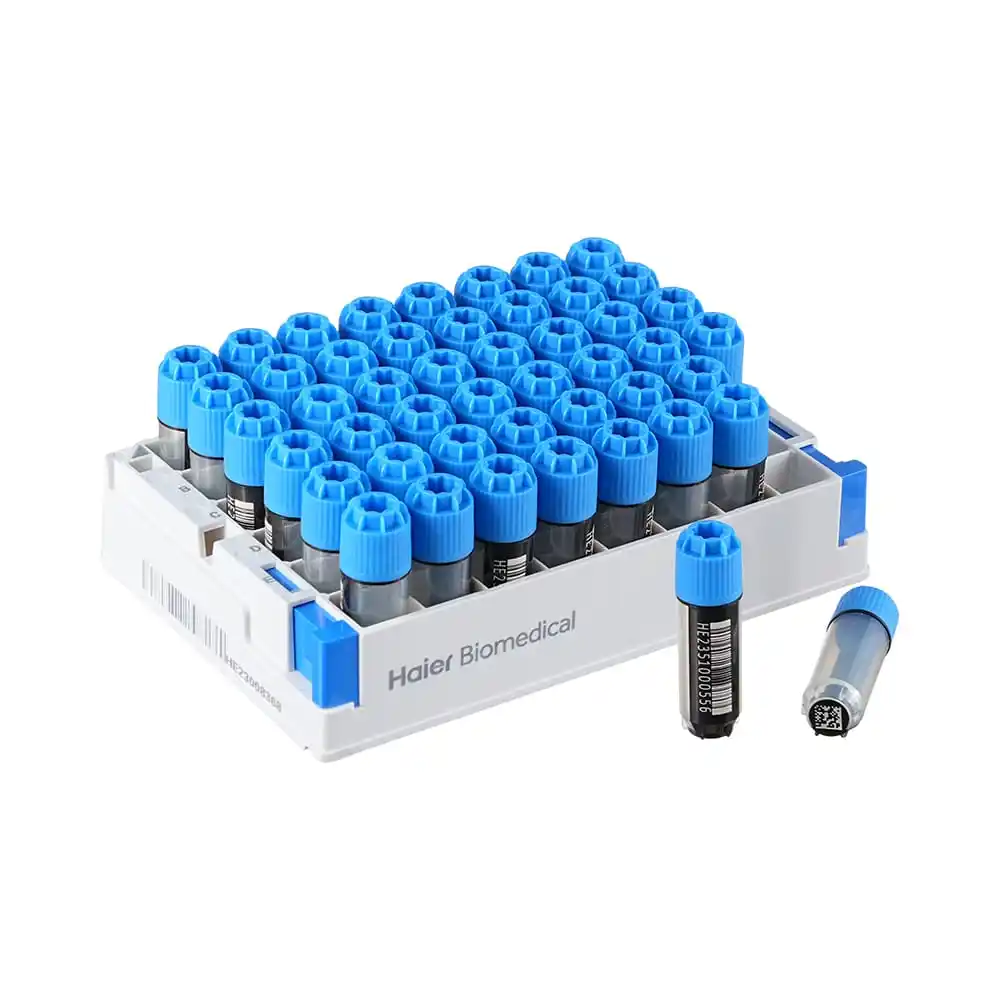
Polypropylene microfuge tubes represent an essential laboratory tool designed for secure sample storage and high-speed centrifugation applications. These specialized containers are engineered from durable polypropylene material, offering scientists and researchers a reliable solution for managing small liquid and solid samples in demanding laboratory environments. Polypropylene microfuge tubes deliver exceptional functionality across multiple research disciplines, including molecular biology, biochemistry, clinical diagnostics, and pharmaceutical testing.
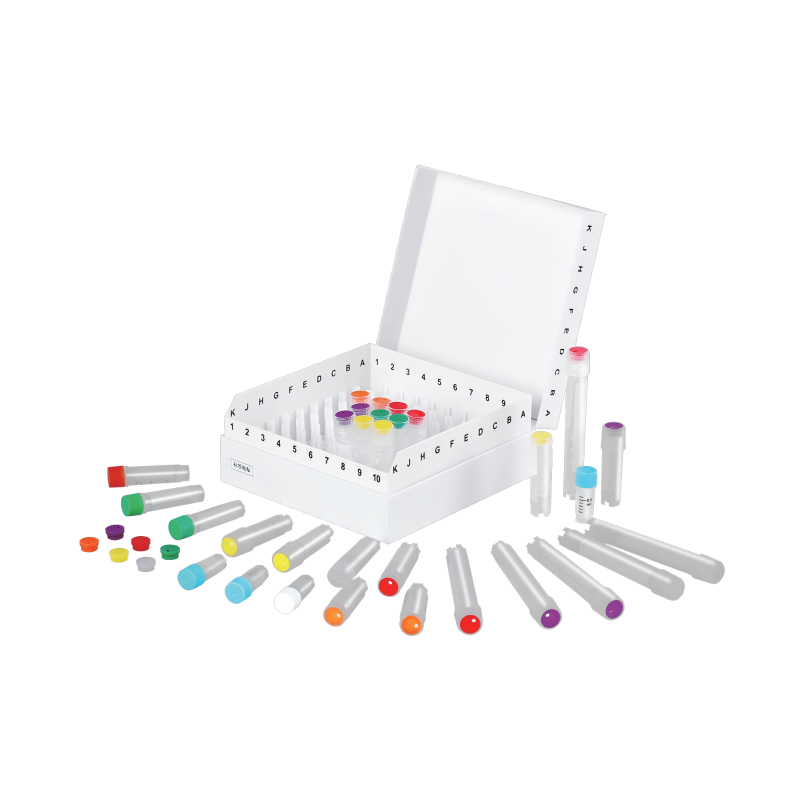
The primary function of polypropylene microfuge tubes involves safely containing and preserving biological samples during centrifugation processes that reach speeds of 15,000 to 20,000 RPM or higher. These tubes feature secure screw caps that prevent sample leakage and contamination during rapid spinning cycles. The transparent design allows researchers to visually monitor sample contents without opening the container, maintaining sample integrity throughout experiments.
Technologically advanced polypropylene microfuge tubes incorporate several sophisticated features that enhance laboratory performance. The tubes withstand extreme temperature fluctuations, ranging from minus 20 degrees Celsius to plus 70 degrees Celsius, making them suitable for freezer storage and high-temperature protocols. Polypropylene microfuge tubes maintain chemical resistance to common solvents and reagents used in analytical work, preventing material degradation or sample contamination. The graduated markings etched on the exterior enable precise volume measurement and tracking, eliminating measurement errors during critical experiments.
Applications for polypropylene microfuge tubes span numerous laboratory settings. Researchers utilize these tubes for DNA and RNA extraction, protein precipitation, blood component separation, vaccine development, and diagnostic testing. Healthcare facilities depend on polypropylene microfuge tubes for microbiological analysis and quality assurance testing. Pharmaceutical companies employ these specialized containers throughout drug development, formulation testing, and stability studies where sample preservation remains critical for research accuracy and regulatory compliance.

 EN